Air-Cooled Crystallizers
Efficient Air Cooling. Controlled Crystallization. Improved Sugar Recovery.
Sattyam Engineers’ Air-Cooled Crystallizers are designed for controlled cooling and further crystallization of massecuite using air as the cooling medium. The system provides effective heat removal, uniform temperature reduction, and controlled crystal growth while minimizing dependence on cooling water. Engineered for reliable sugar mill operation, these crystallizers support improved exhaustion, enhanced sugar recovery, efficient crystallization, and dependable performance under continuous processing conditions.
Key Features
- Efficient air-based cooling
- Controlled massecuite cooling
- Uniform temperature reduction
- Better exhaustion of mother liquor
- Reduced cooling-water consumption
- Optimized massecuite circulation
- Robust industrial construction
- Easy operation and maintenance
Types of Air-Cooled Crystallizers
They ensure uniform crystal growth, effective heat transfer, improved sugar recovery, reduced water consumption, energy-efficient operation, and reliable performance for modern sugar processing applications.
Designed in a vertical configuration for efficient cooling and crystallization of massecuite, this system provides controlled air circulation and optimized temperature reduction while requiring minimal floor space.
Key Benefits:
- Compact installation
- Efficient air circulation
- Controlled cooling
- Uniform crystallization
- Reduced water requirements
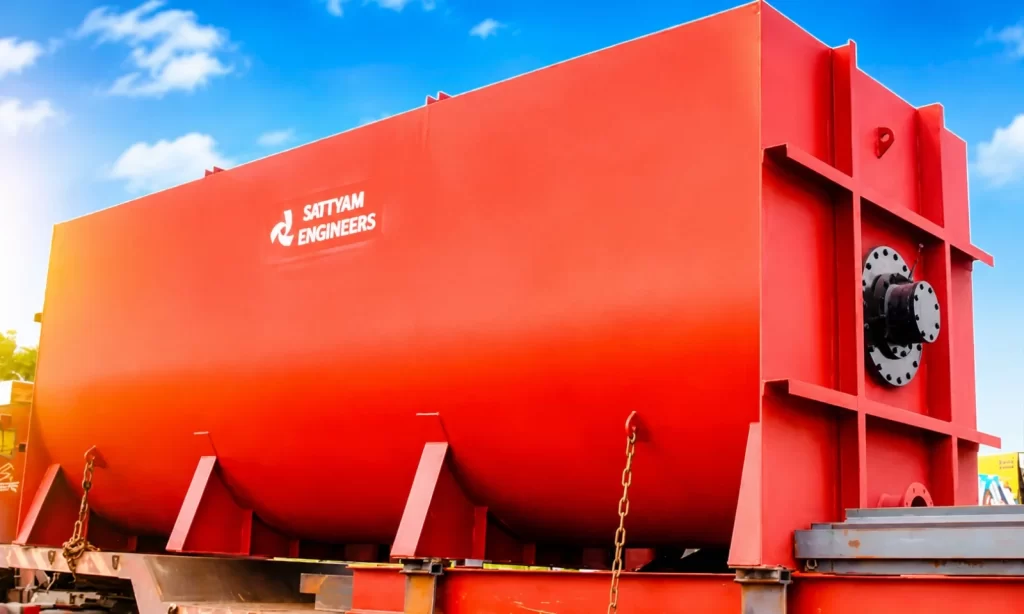
Designed for effective massecuite cooling in a horizontal arrangement, this crystallizer provides controlled heat removal and consistent massecuite movement for efficient secondary crystallization.
Key Benefits:
- Efficient cooling
- Uniform massecuite movement
- Effective heat transfer
- Consistent crystal development
- Easy accessibility
Equipped with a controlled forced-air circulation system, this configuration enhances heat removal from massecuite and provides stable cooling conditions for improved crystallization and sugar recovery.
Key Benefits:
- Enhanced cooling efficiency
- Controlled airflow
- Faster heat removal
- Consistent crystallization
- Improved sugar recovery
Why Choose Sattyam Engineers?
Choosing Sattyam Engineers means choosing dependable air-cooling technology engineered for efficient crystallization and sugar recovery. Our Air-Cooled Crystallizers combine optimized airflow, effective heat transfer, controlled cooling and robust construction to deliver consistent performance while reducing reliance on cooling water.